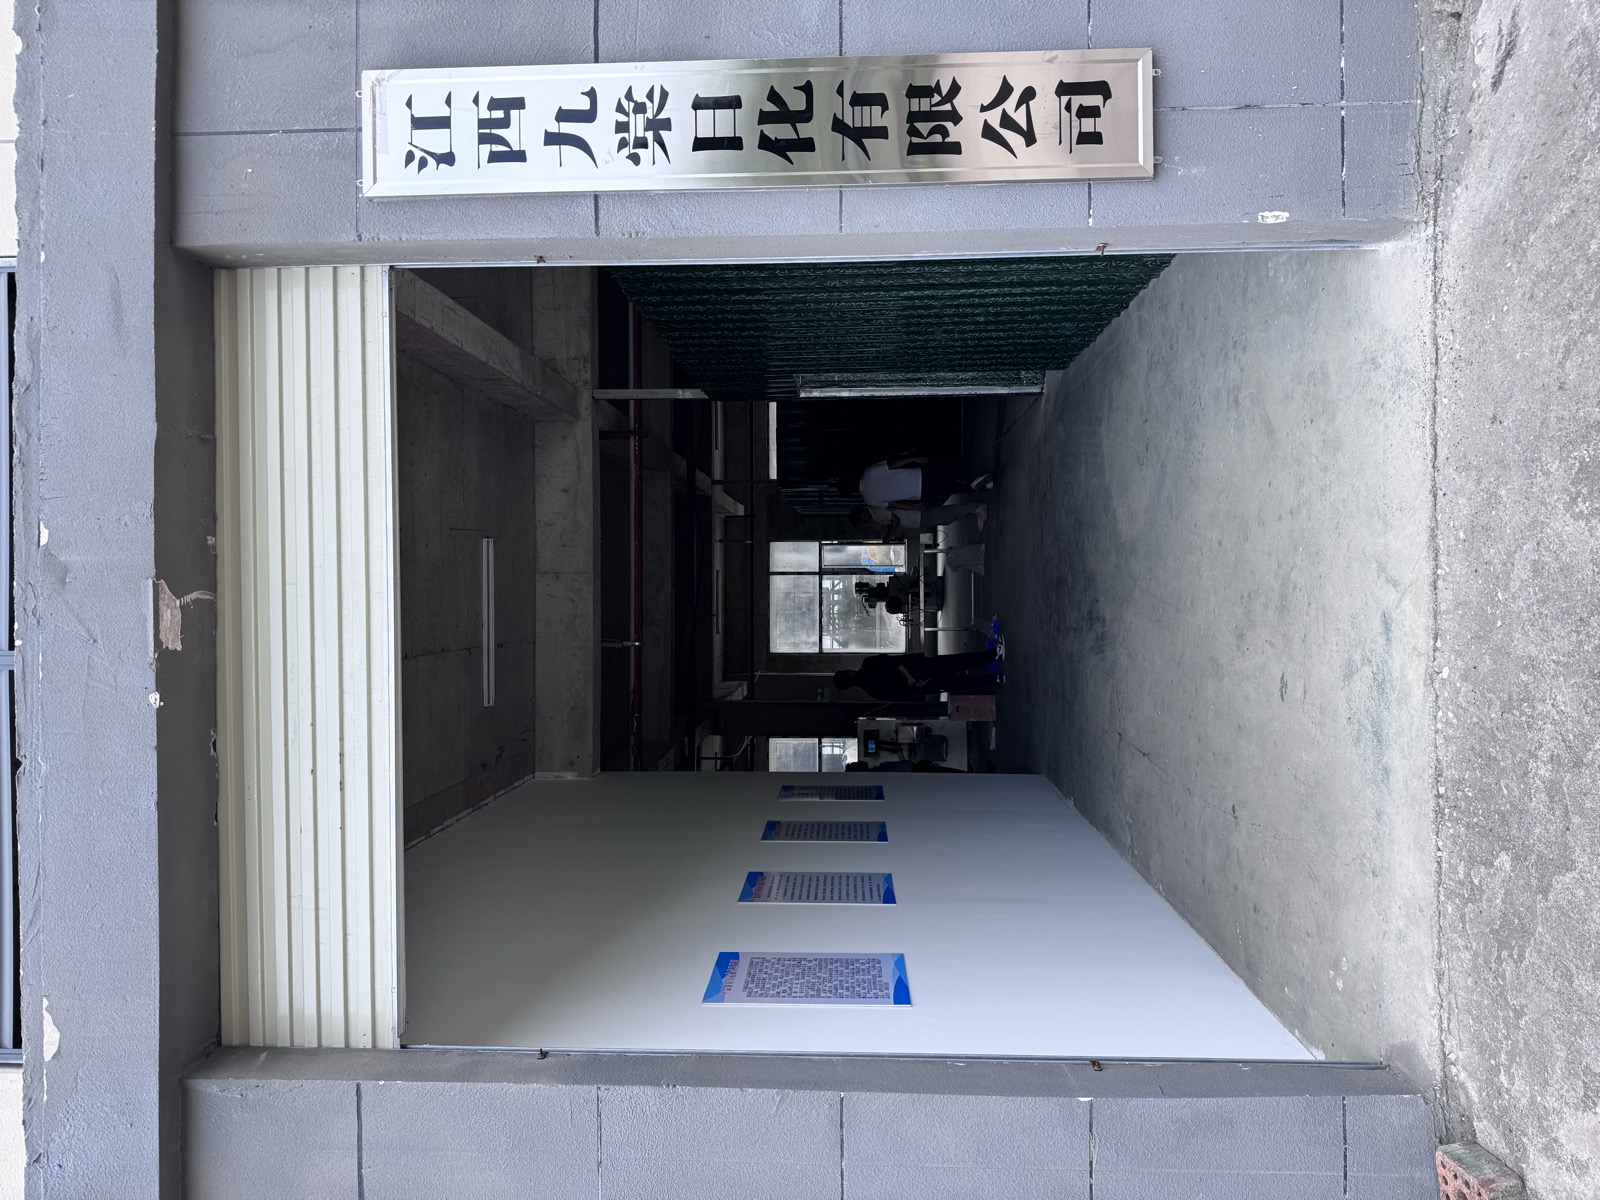
A 3,000 m² manufacturing plant in Jiangxi Province with full in-house production, QC and export packaging.
Our manufacturing plant is located in the West Zone of the Industrial Park in Yongfeng County, Ji'an City — a well-established industrial area in central Jiangxi Province with good logistics access to major ports in eastern China.
The facility covers 3,000 m² of production and warehouse space. Since commencing operations in 2012, we have steadily expanded our production lines to handle synthetic camphor balls (p-dichlorobenzene), naphthalene mothballs, and mildew prevention tablets under one roof.
Today we operate with significant monthly output and serve both the domestic Chinese market and growing export volumes across Southeast Asia.
From raw chemical input to sealed export-ready bags — every step happens in our own facility.
Key chemical inputs — p-dichlorobenzene, naphthalene, binders and additives — are sourced from qualified domestic suppliers and inspected on arrival.
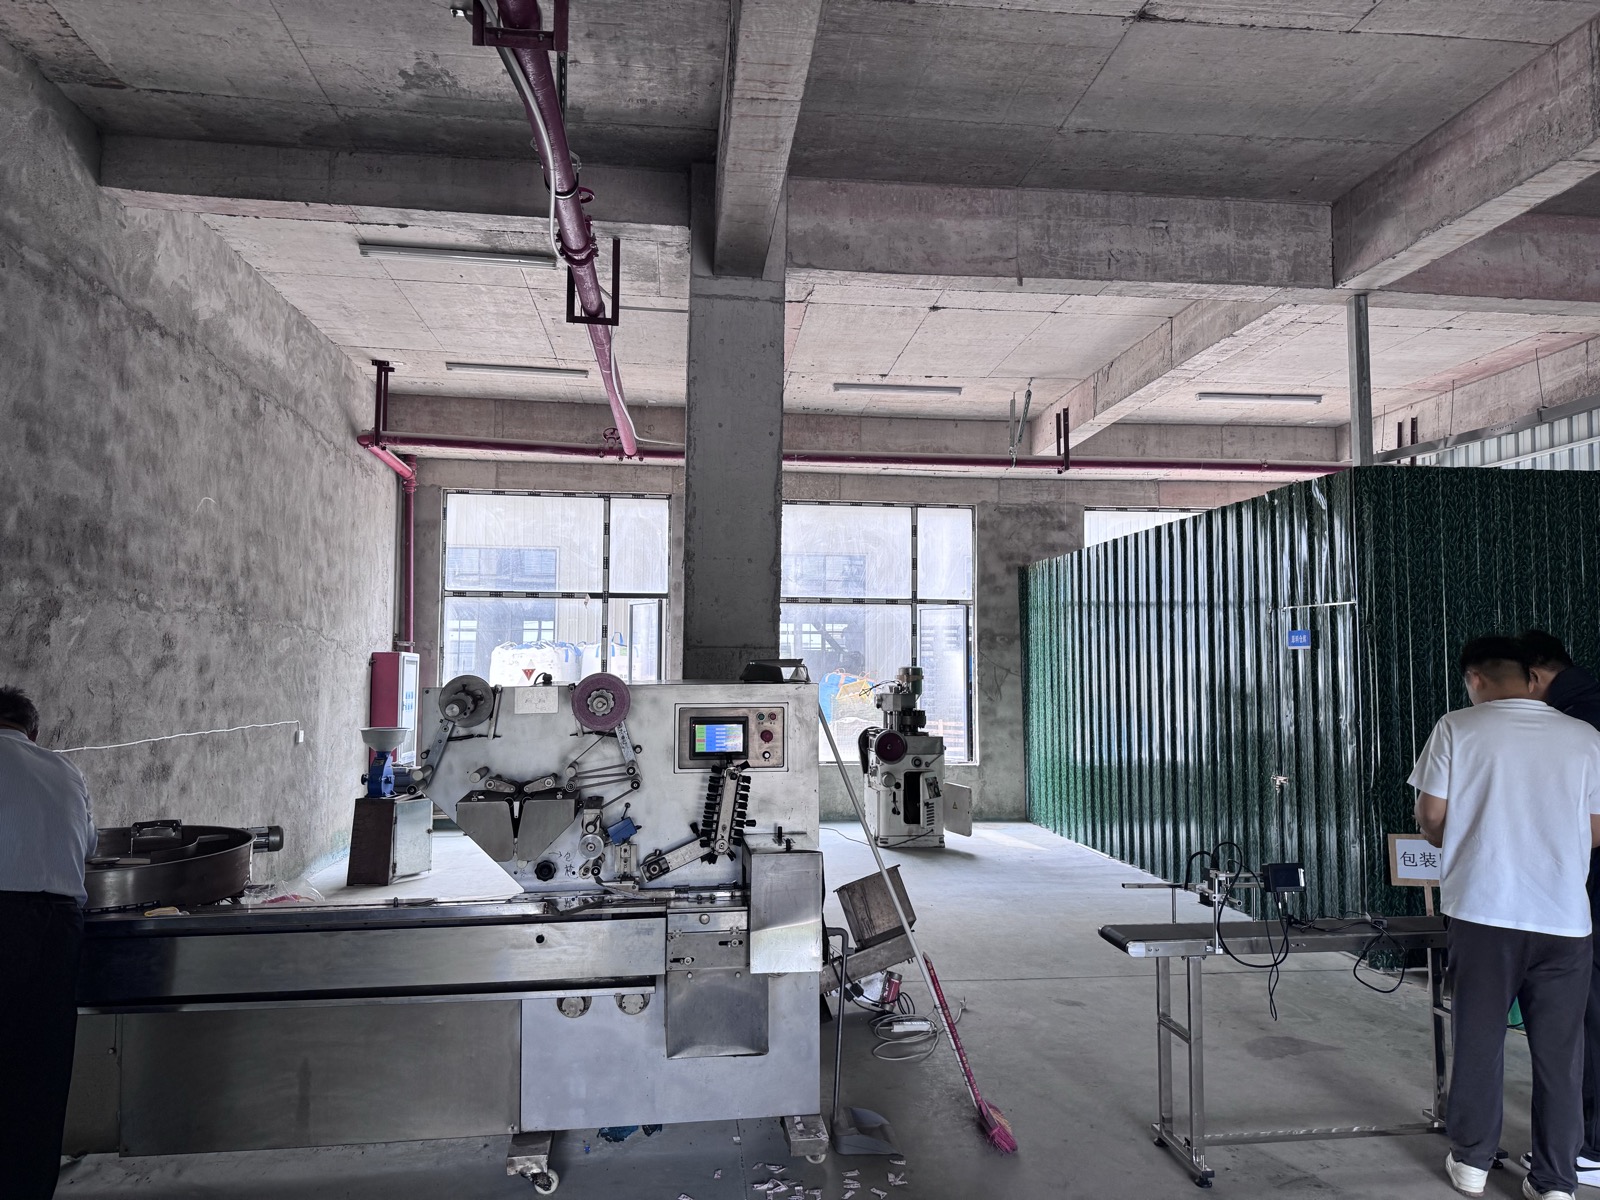
Raw materials are precisely weighed, blended in controlled mixers, and pressed or granulated into balls, tablets or custom shapes.
In-line sampling checks weight, appearance and consistency. Finished batches go through lab testing before approval for packaging.
Products are bagged in standard 30g / 150g / 235g / 500g sizes or custom formats, cartoned, palleted and prepared for international shipping.
Consistent quality is non-negotiable — here's how we ensure it for every shipment.
Every batch of raw material is tested upon delivery to verify purity, moisture content and specification compliance before it enters production.
Production operators and QC staff carry out weight, density and appearance checks at regular intervals during each shift.
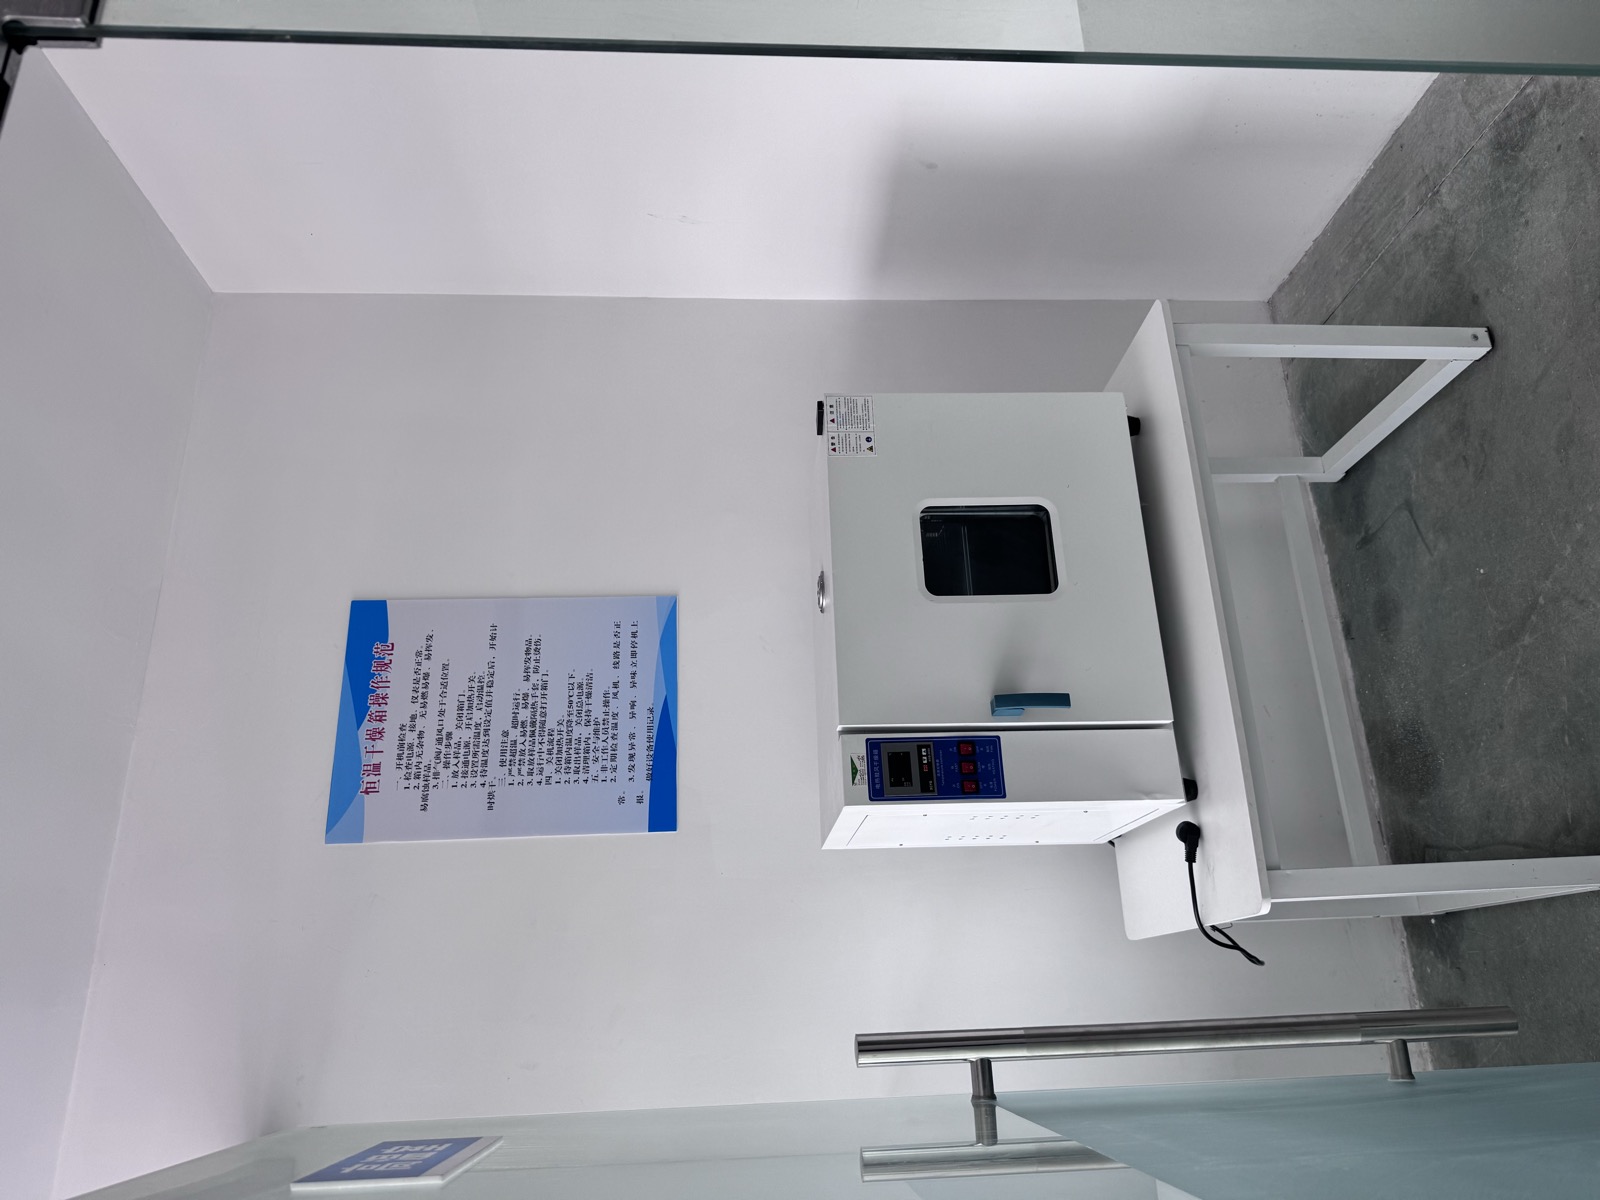
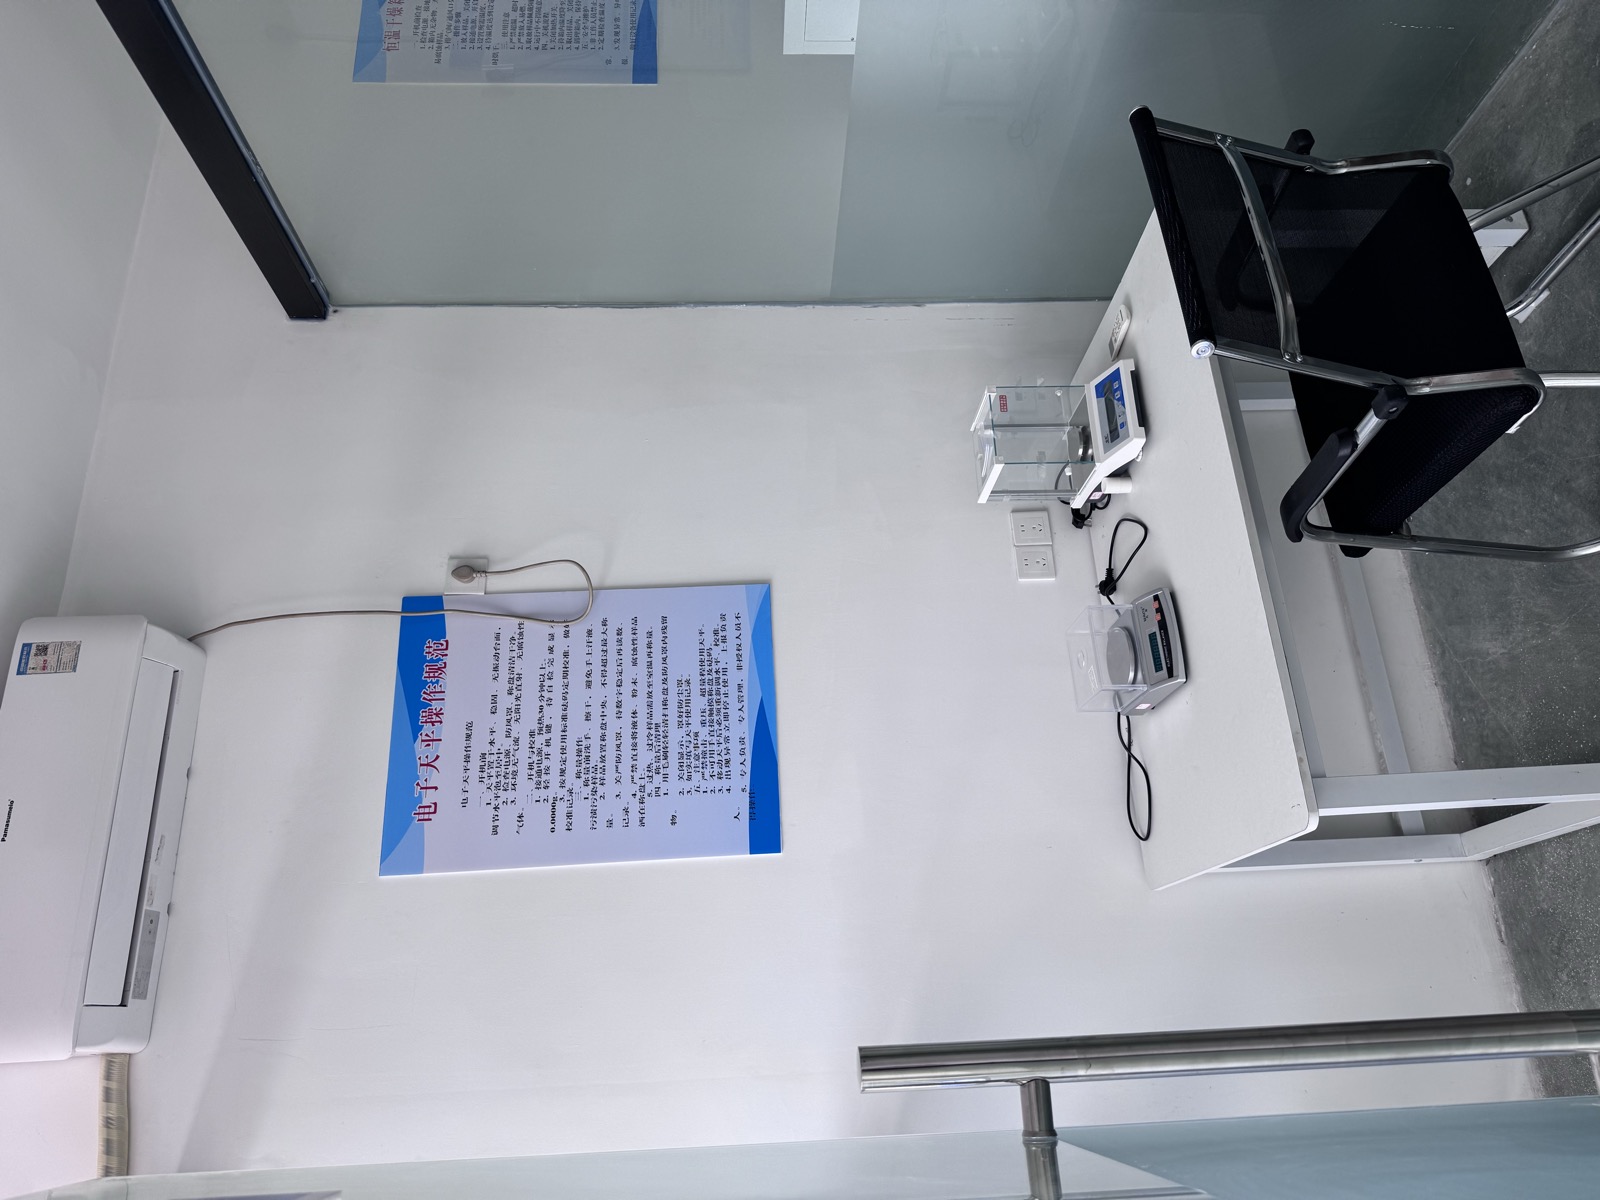
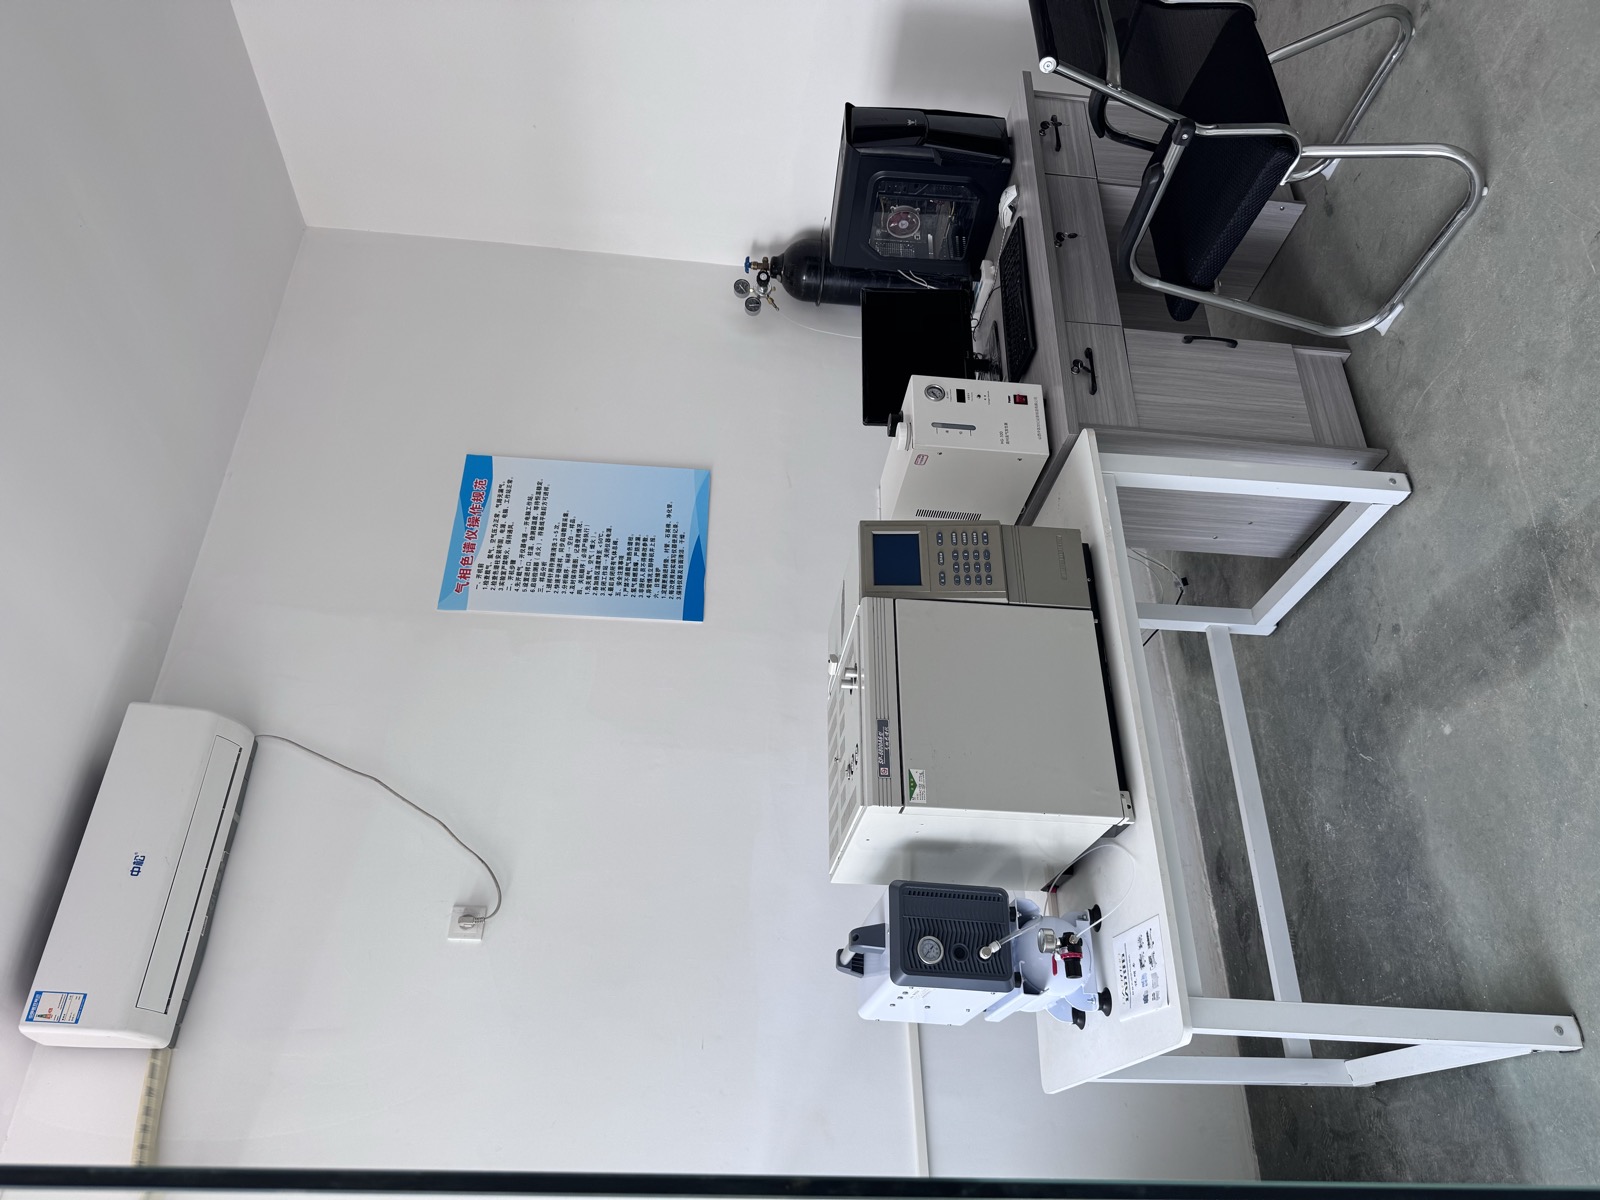
Each finished batch is tested in our on-site lab for active ingredient content and physical properties before release for packaging.
Every production run is logged with batch numbers, material suppliers and test results — full traceability from shelf to source.
We are actively working toward formal ISO certification as part of our ongoing commitment to quality management.
A visual tour of key production areas within our facility.
Built for reliable, scalable production of household chemical products.
Dedicated production areas for each product line with separate material handling to prevent cross-contamination.
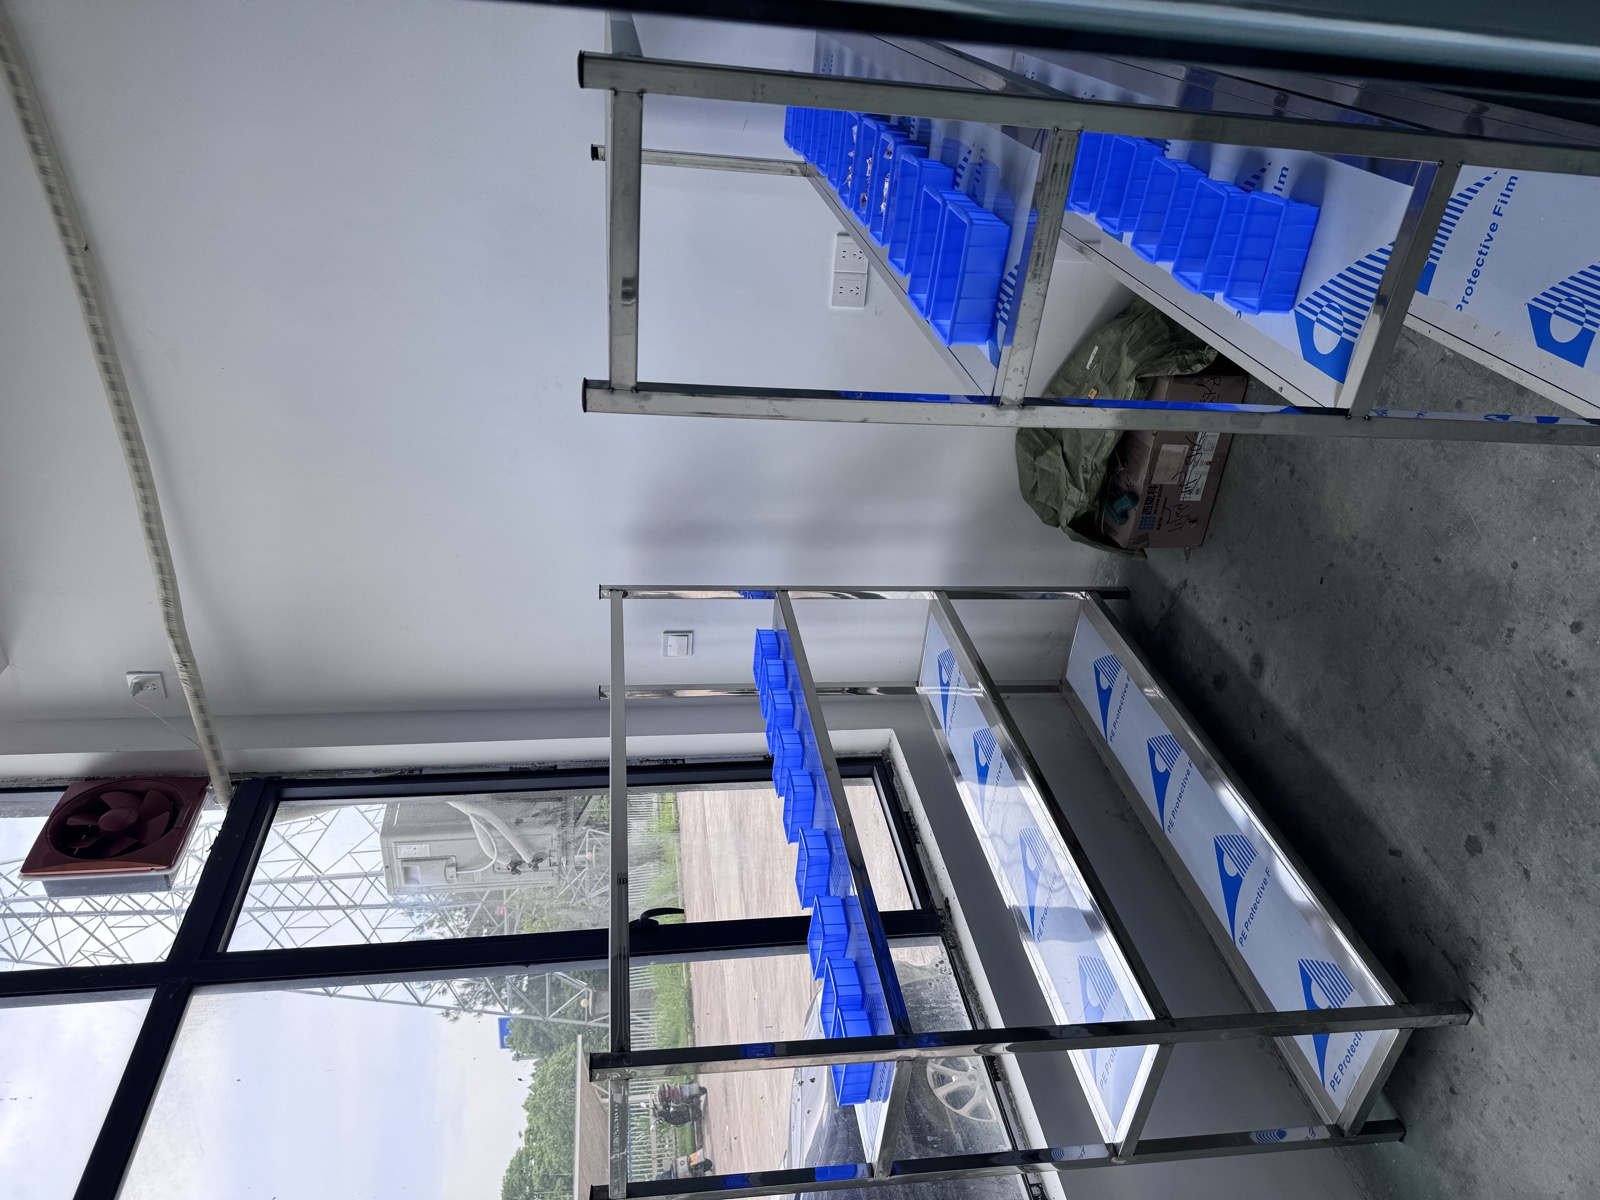
Climate-aware storage for raw materials and finished goods, with separate zones for quality hold and released stock.
Loading docks and export staging area. Experienced in FCL, LCL and mixed-container shipments to SEA ports.
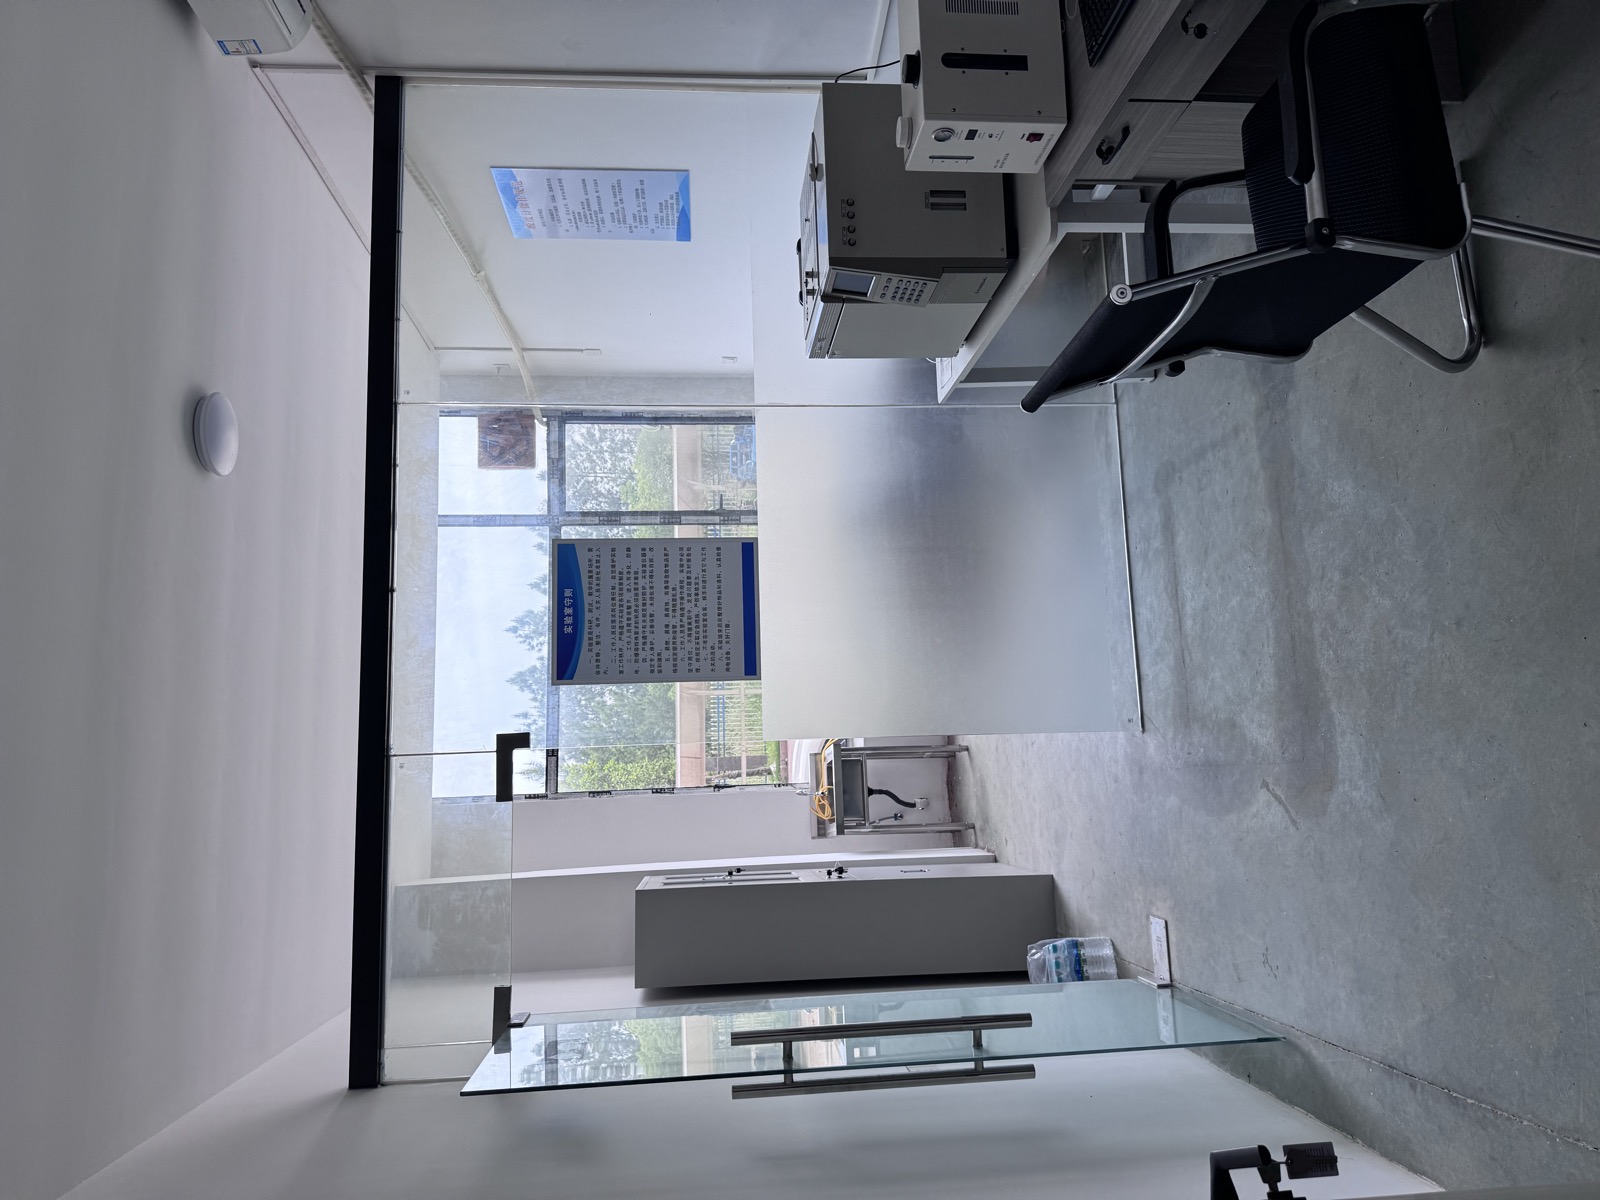
In-house quality control laboratory with basic analytical equipment for batch verification and troubleshooting.
Full-time engineering and maintenance staff to minimize downtime and keep all lines running efficiently.
Rigorous safety protocols, worker PPE, and proper chemical handling procedures throughout the facility.